A batch that looks flawless can still leak at the neck. On our Taizhou line, PET bottle neck/thread standards decide whether ten thousand caps seal perfectly or fail in transit.
To avoid supplier mismatches, specify the full PET bottle neck/thread standard by name and revision—such as PCO 1881, GME 30.40, or 24/410—plus a dimensioned drawing covering T, E, I, S, and H, thread starts, and pitch. Then validate bottle and closure together before mold approval.
That one sentence hides years of costly lessons. Bottles that look identical can fail at the finish level. Below, I break the problem into four practical steps: identify the finish, confirm the thread standard, prevent cap mismatches, and demand the right documents.
How do I identify the right neck finish size for my PET bottle order?
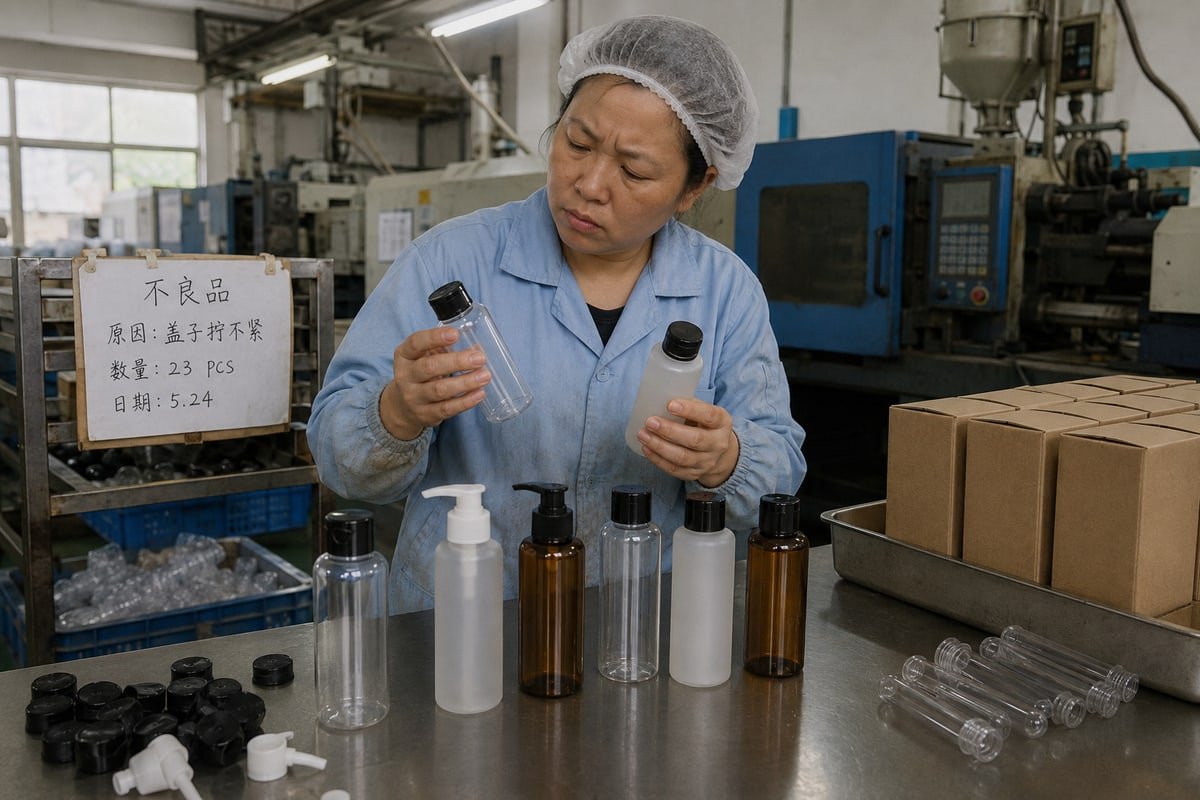
Last spring, our QC team rejected a preform batch that measured 28 mm on the caliper yet cross-threaded every cap. The nominal size was right; the finish family was wrong.
Identify the neck finish by matching three data points: the nominal diameter, the named finish standard (such as PCO 1881, 24/410, or EN 16594), and the closure system it must fit. Measure T, E, and H dimensions on an existing sample, then confirm against the official finish data sheet.
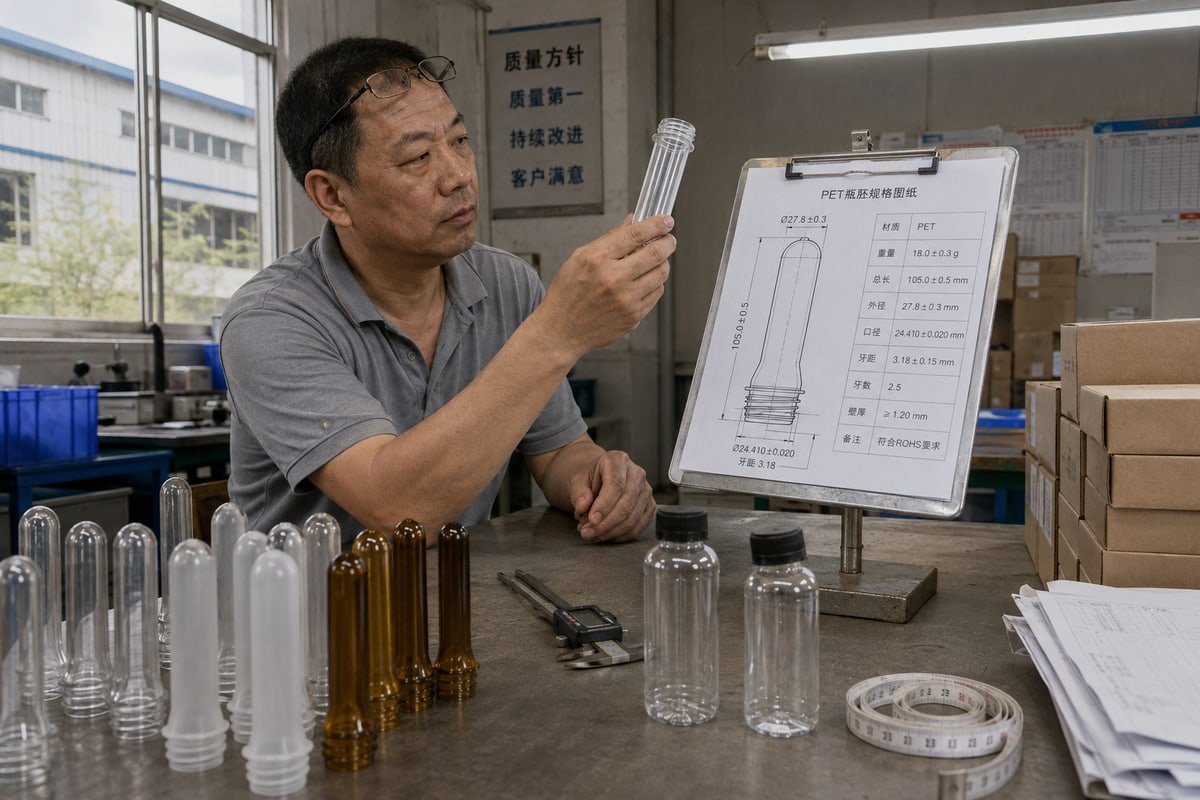
The core mistake I see from new buyers is treating neck size as one number. It is not. A nominal diameter is a family label. Inside that family sit several distinct geometries. Each has its own thread profile, height, and sealing design.
Why 28 mm Is Not Enough
Take the famous 28 mm example. That label can refer to PCO 1810, PCO 1881, or a 28/410 cosmetic finish. All three are "28 mm." None of them interchange. The PCO 1881 vs 1810 comparison is the classic trap: PCO 1881 is a shorter, lighter successor to the older PCO 1810 neck 1, and caps for one will not seal reliably on the other. This is exactly why standards bodies publish full geometry, not just diameter. ISBT neck finish standards govern the PCO family for beverage interchangeability, CETIE maintains GME data sheets 2 such as 26/22, 29/25, 47/41, and snap-on variants, and older BPF finish specifications still circulate in some markets. In our cosmetic and skincare world, the SPI-style 410 series (20/410, 24/410, 28/410) dominates pumps and disc caps.
Match the Finish Family to Your Product
| Standard | Nominal Size | Key Detail | Typical Use |
|---|---|---|---|
| EN 16068 | 38 mm | Three thread starts, 120° apart, 9 mm lead per turn | Flat water, non-carbonated drinks |
| EN 16594 | 26 mm | Three-start PET screw finish | Flat waters, non-carbonated beverages |
| EN 16592 | 29 mm | Three-start PET screw finish | Flat waters, non-carbonated beverages |
| EN 16065 | 30/25 low | Three-start low finish | Lightweight water bottles |
| PCO 1881 | 28 mm | Shorter, lighter successor to PCO 1810 | Carbonated and still beverages |
| 24/410 & 28/410 | 24–28 mm | SPI-style continuous thread | Lotions, pumps, cosmetic closures |
So before you order, name the standard. Never quote the diameter alone.
What thread standards should I confirm before approving a supplier's mold?
Every mold approval forces a trade-off we weigh carefully in Taizhou: sign off fast to protect lead times, or slow down and verify every thread dimension first.
Before approving a mold, confirm the thread standard name and revision, number of thread starts, thread pitch and lead, sealing surface geometry, bore diameter, finish height, support ledge position, and tamper evident bead dimensions. Require the supplier to quote the exact ISBT, CETIE, or EN reference in writing.
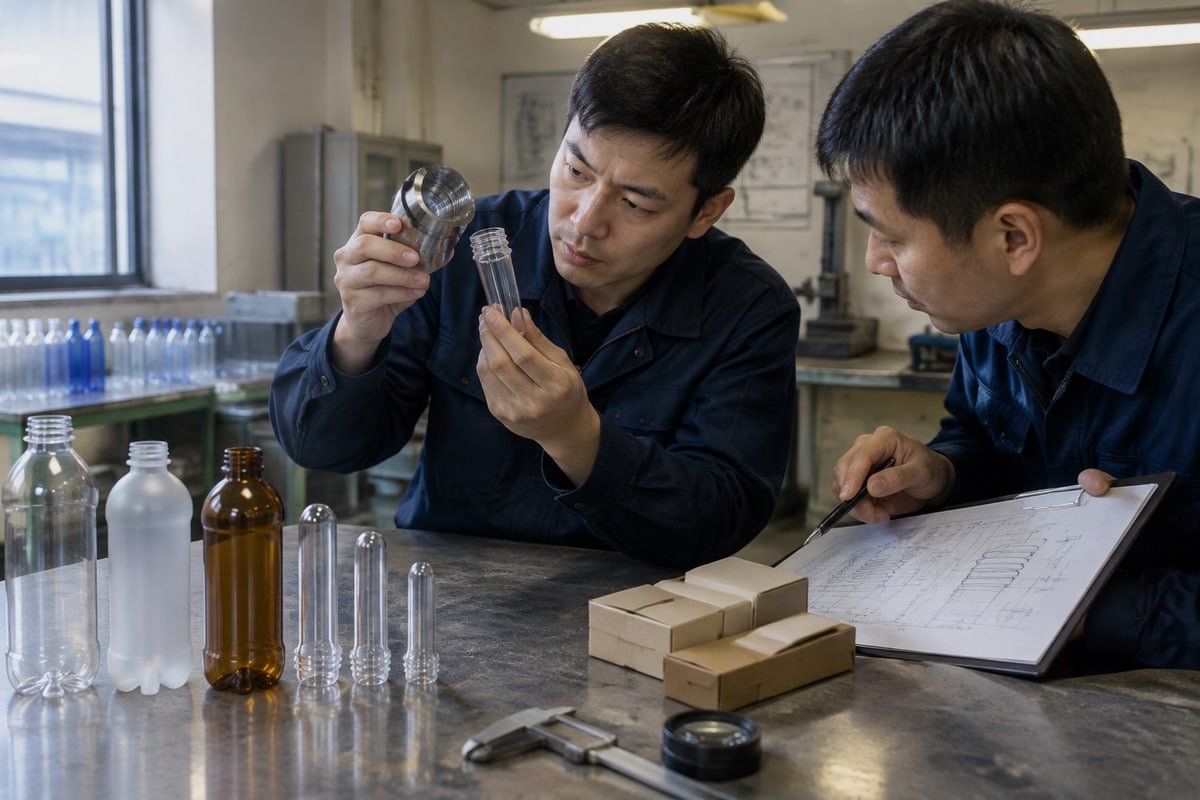
Mold steel does not forgive guesses. Once tooling is cut, every dimensional assumption is frozen into thousands of bottles. That is why we treat thread confirmation as an engineering gate, not a formality.
The Five Critical Letters
Every serious specification document should define five dimensions. These letters appear on proper finish data sheets and on our own preform neck dimensions reports.
| Dimension | Meaning | Why It Matters |
|---|---|---|
| T | Thread outside diameter | Controls thread engagement depth with the cap |
| E | Outside diameter below thread | Affects tamper band and cap skirt clearance |
| I | Inner bore diameter | Governs plug seals, liners, and fill nozzles |
| S | Start of thread position | Sets cap orientation and prevents cross-threading |
| H | Finish height | Determines seal compression and capper setup |
Thread Starts, Pitch, and Lead
Thread starts change everything about application speed. EN 16068, for example, defines a 38 mm finish with three thread starts spaced 120° apart and a 9 mm lead per turn. A three-start finish seats the cap in roughly one-third of a turn compared to a single-start thread. If your capper is set for one geometry and the bottle arrives with another, closure application torque 3 readings drift immediately. Confirm thread pitch and lead explicitly, because two finishes can share a diameter yet differ in lead angle, which causes cross-threading at high speed.
Watch the Tethered Cap Transition
For European-bound products, check GME 30.40. The tethered cap regulation requires specific neck-ring modifications 4 to hold the hinge mechanism. Also confirm which CETIE data sheet revision the supplier is using; these sheets get updated, and an old revision can quietly change the bottle cap sealing surface your mold produces.
How can I avoid cap compatibility issues caused by neck/thread mismatches?
An Australian procurement manager once messaged us on WhatsApp: her lotion caps sealed in Sydney but leaked after air freight. The culprit was a tiny sealing-surface mismatch.
Avoid cap compatibility issues by validating bottle and closure as one matched system: run tolerance stack-up analysis, test closure application torque and removal torque, perform leak and fit trials with production caps, and complete a capping-line trial before releasing molds for mass production.
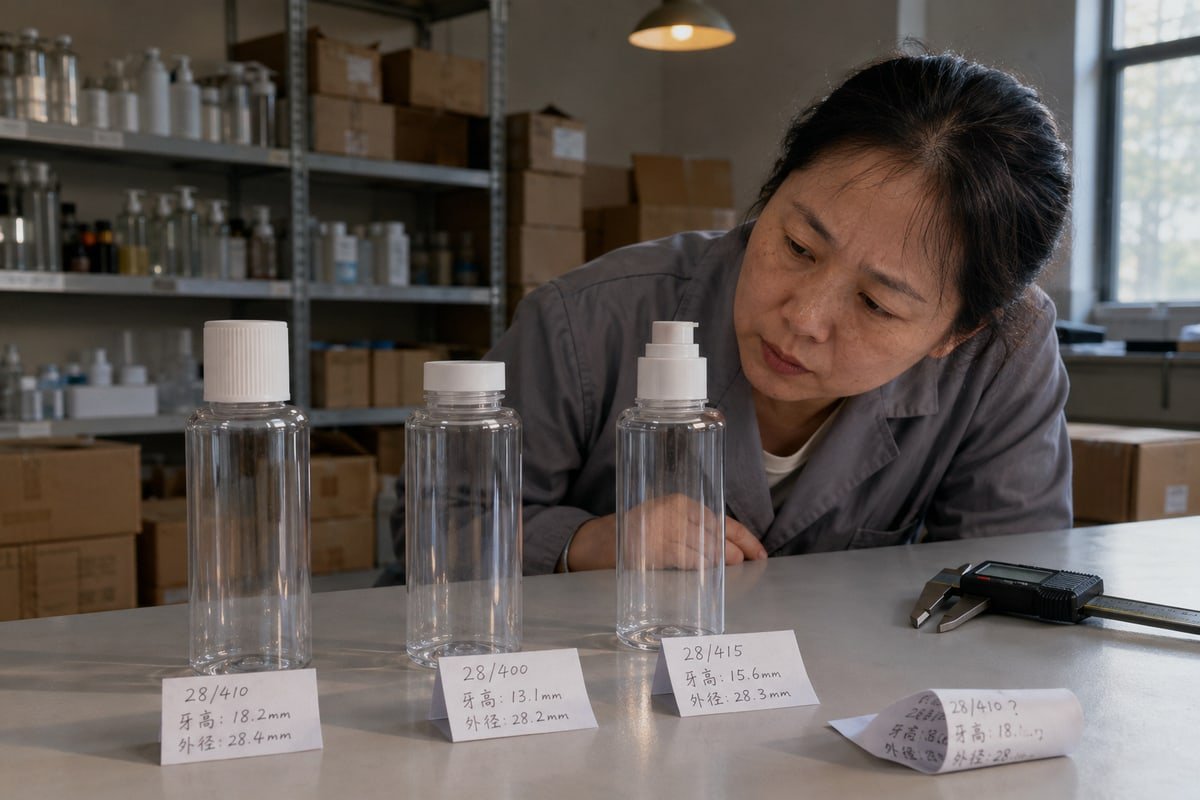
Buyers often assume a slightly different finish is acceptable because the plastic cap will "flex to fit." I push back on this every time. Relying on deformation destroys your sealing margin, and the failure only appears later as leaks, returns, and chargebacks. Here is the validation workflow we run before any mass production release:
- Tolerance stack-up analysis. Check that the maximum material condition of the bottle neck still fits the minimum material condition of the closure. Two parts can each pass inspection and still bind together at the extremes.
- Fit-for-purpose sample test. Apply a real batch of production closures to the actual preform neck, not a lookalike. This catches tamper evident ring compatibility problems before tooling commitment.
- Torque testing. Measure closure application torque and removal torque against target windows. Drifting torque is the earliest warning of thread geometry mismatch.
- Leak and seal testing. Run vacuum or pressure leak tests, plus inverted transit simulation for lotions and serums.
- Dynamic line trial. Lightweighted necks can pass static checks yet ovalize under capping pressure. High-speed camera verification on the capping line catches this ovalization that calipers never see.
- Material check. If you use rPET, verify neck crystallization and dimensional stability. Higher recycled content can cause unexpected thermal shrinkage during injection stretch blow molding, shifting finished neck dimensions.
One more warning: never reuse an old cap tooling or preform mold for a "similar" finish without re-running this workflow.
What documentation should I request from suppliers to verify neck/thread specs?
One hard lesson shaped our export paperwork: a drawing without a revision number is an invitation for a supplier to guess. We now freeze every spec before tooling.
Request a dimensioned neck finish technical drawing with tolerances and revision number, the official finish data sheet reference, a first-article inspection report, material and rPET declarations, closure compatibility confirmation, and torque and leak test results. Freeze the drawing revision in writing before production release.
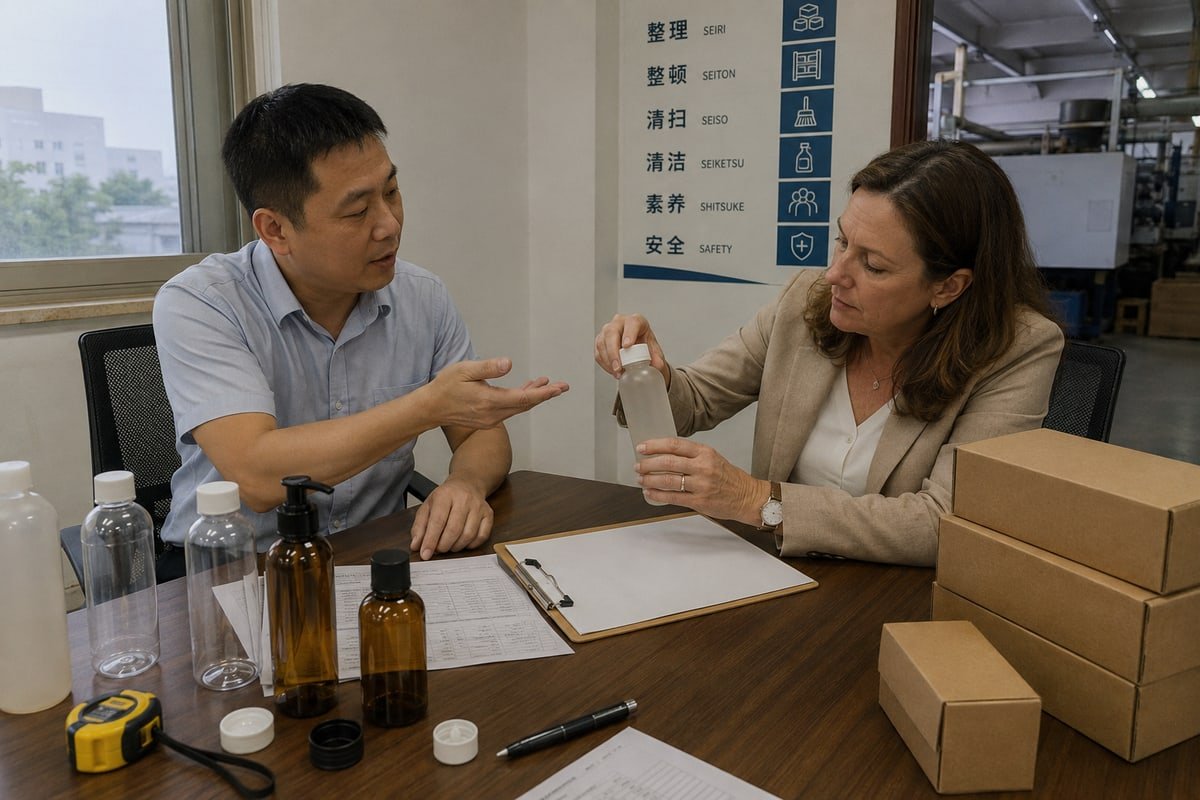
Documents are cheap insurance. A leaking container shipment is not. When we onboard a new closure vendor for our custom cosmetic packaging projects, we exchange the same document pack we expect our own buyers to demand from us. Here is the complete list, in the order you should collect it:
| Document | What It Must Contain | When to Collect |
|---|---|---|
| Neck finish technical drawings | T, E, I, S, H with tolerances, thread starts, pitch, and revision number | Before quoting |
| Standard declaration | Whether the finish is standard, modified standard, or custom, with the exact ISBT, CETIE, EN, or BPF reference | Before quoting |
| First-article inspection report | Measured dimensions of actual first samples against the drawing | Before mold approval |
| Closure compatibility confirmation | Written statement naming the approved cap standard and supplier | Before mold approval |
| Material and rPET declaration | Resin grade, recycled content ratio, shrinkage allowance | Before mold approval |
| Test reports | Torque, leak, fit, and capping-line trial results | Before mass production |
| Revision freeze letter | Signed confirmation locking the drawing revision across bottle, preform, cap, and capper suppliers | Before production release |
Why Revision Control Matters Most
Standards bodies revise their finish data sheets. If your bottle maker works from an updated CETIE sheet while your cap vendor holds an older version, both suppliers are "compliant" and your parts still mismatch. Lock one revision across every party in the chain.
Standard, Modified, or Custom?
Procurement often chases the cheapest quote, while engineering needs exact control. Resolve this tension in writing. A standard finish keeps cap sourcing flexible; a custom neck may serve dispensing or branding needs, but it locks you to fewer vendors. Make the supplier declare which one you are buying.
Conclusion
Never buy PET bottles by diameter alone. Name the standard, lock the drawing, and validate bottle plus cap as one system—or a leaking shipment will teach you instead.
Footnotes
1. Authoritative source for the PCO 1810 and 1881 standards used globally for carbonated beverage bottle finishes. ↩︎
2. International center providing standardized GME finish geometries to ensure compatibility between glass or PET containers and closures. ↩︎
3. Global standards federation providing technical specifications for measuring the application and removal torque of threaded closures. ↩︎
4. European Commission environment portal explaining the legislative requirements for tethered caps on single-use plastic beverage containers. ↩︎
