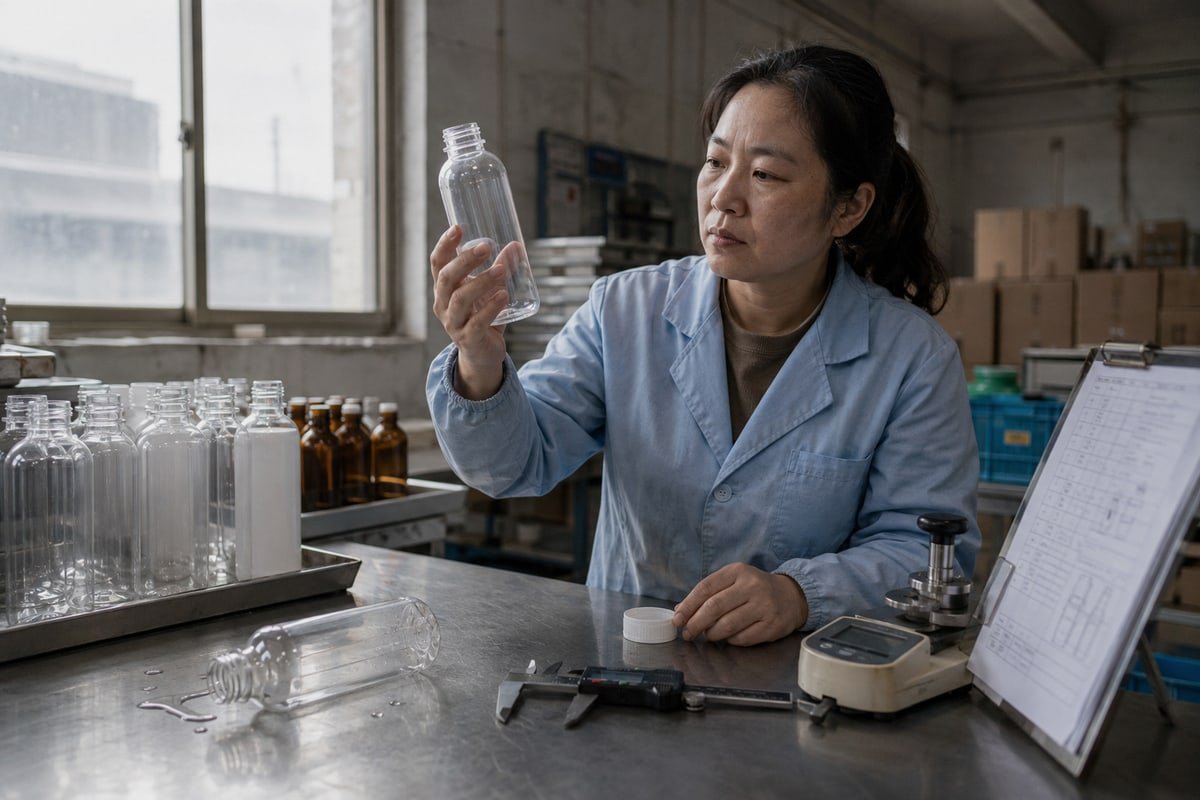
A whole container of leaking bottles starts with one wrong cap vacuum leak performance 1. Before any PET bottle leaves our Taizhou line, we confirm bottle neck size against the exact cap specification.
To confirm bottle neck size matches your caps, verify that both parts share the same neck finish code (like 24-410), measure the T dimension across the thread peaks with calipers, compare drawings against GPI/SPI standards, and test physical samples for torque and leaks before bulk production.
That answer sounds simple. In practice, most cap failures come from small details buyers skip. This guide walks through each step, in the order we use it ourselves.
How do I measure the neck finish of a PET bottle correctly before ordering?
A few years back, our QC team caught a batch where every bottle "measured 24mm" by eye but failed the caliper check. That day changed how I teach buyers to measure.
Measure the T dimension — the outside diameter across the outermost thread peaks — with digital calipers at three points around the neck. Then record the E dimension (neck wall without threads), the H dimension (neck height), and the I dimension (inner diameter), averaging results across several bottles.
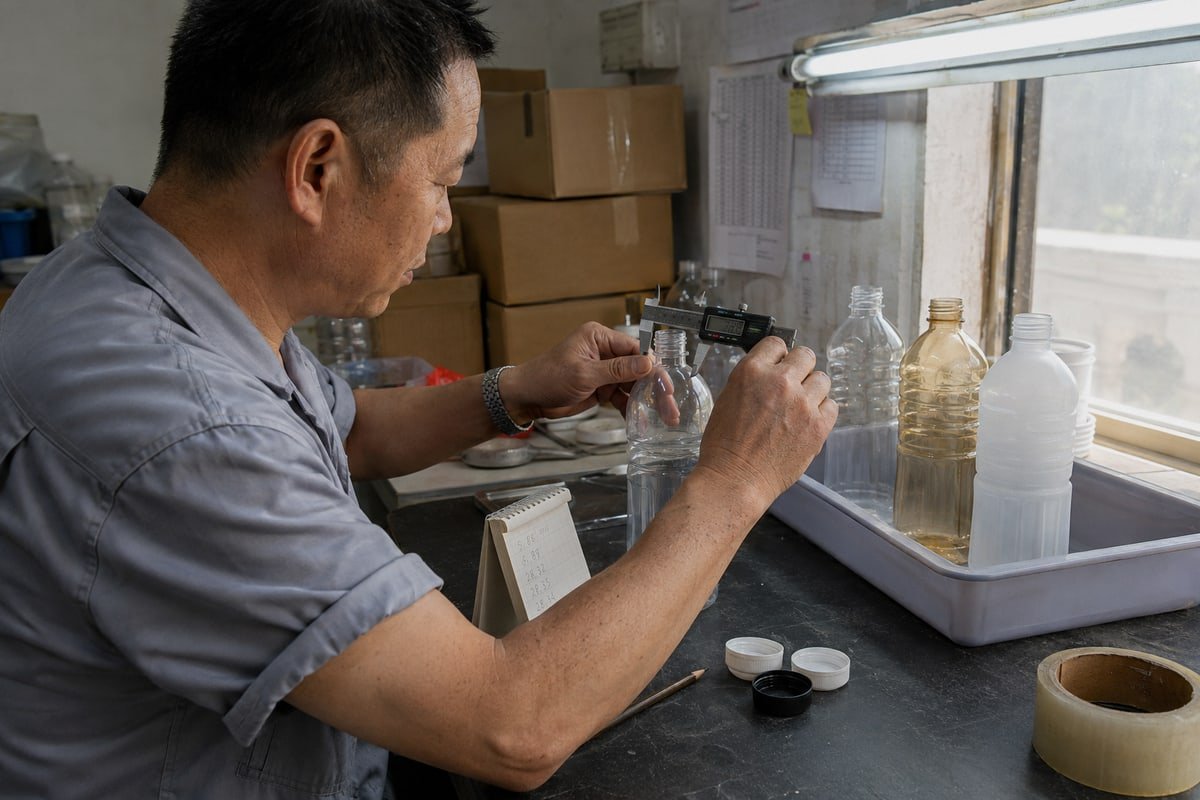
The single most common mistake I see is measuring the bottle opening instead of the threads. The neck diameter T dimension is taken across the widest points of the thread peaks. If you measure only the mouth, you will pick a cap that is too small, and it will cross-thread on the line.
The four dimensions that matter
| Dimension | What it means | How to measure it |
|---|---|---|
| T | Outside diameter across thread peaks | Calipers across the outermost thread points, at 3 spots around the neck |
| E | Outside diameter of the neck wall, excluding threads | Calipers on the smooth wall between thread roots |
| H | Neck height from the top of the finish to the shoulder intersection | Depth gauge or calipers held vertically |
| I | Inner diameter of the neck opening | Inside jaws of the calipers across the bore |
The neck height H dimension matters more than people expect. If H is too short, the cap bottoms out before the liner compresses. If it is too long, thread engagement depth suffers and the cap sits loose.
Why one bottle is never enough
PET bottles are blow molded, so small variation between cavities is normal. On our line, we always measure five to ten bottles and average the readings. Take each reading at multiple points around the circumference, because necks are rarely perfect circles. Thread pitch measurement also helps: check the spacing between thread turns and compare it to the cap drawing. If your supplier cannot give you a neck drawing, that variation is exactly why you should insist on multiple physical samples before ordering.
What neck size standards should I check to avoid cap mismatch issues?
An Australian procurement manager once messaged me on WhatsApp: "Your bottle is 28mm, my cap is 28mm, why does it leak?" The answer sits in the second half of the code.
Check the two-part neck finish code, such as 28-410, where the first number is the neck diameter in millimeters and the second identifies the thread style. Cross-reference both bottle and cap against GPI or SPI finish dimension charts, and confirm tethered-cap rules where they apply.
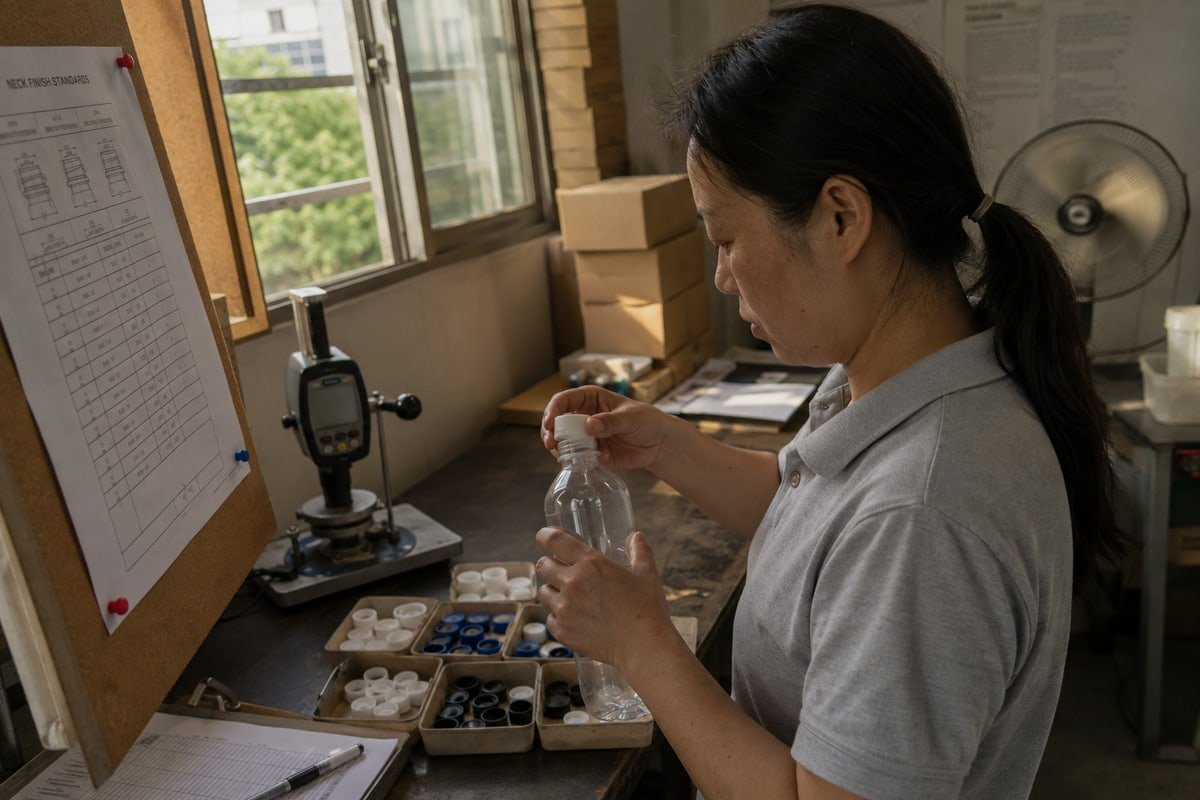
A "28mm bottle" is not one thing. It could be a 28-400, a 28-410, or a 28-415, and those three caps are not interchangeable. GPI neck finish standards and SPI finish dimensions exist precisely to solve this. The first number is the T diameter. The second number defines the thread configuration for continuous thread closures.
Quick reference for common finish codes
| Finish code | Thread turns | Typical use |
|---|---|---|
| 400 series | 1 full turn | Jars, short caps, wide openings |
| 410 series | 1.5 turns | Lotion pumps, taller skincare closures |
| 415 series | 2 full turns | Droppers, tall slim necks |
You can even verify the style by hand: count the thread revolutions on the neck. One full turn points to a 400 finish, one and a half turns points to a 410, and two full turns points to a 415. When a client sends us a cap for matching, this count is the first thing our engineers check. A 28-410 closure size on a 28-400 neck will spin on but never seal, because the thread engagement depth and cap skirt height are different.
Two more checks belong on your list. First, if you sell beverages into the EU, Directive 2019/904 3 requires tethered caps, and tethered closures need specific neck geometries to hold the cap on. Second, confirm the tamper-ring locking diameter on the bottle matches the cap's tamper band, or your tamper-evident seal compatibility fails even when the threads fit.
Can I request samples to test cap compatibility before bulk production?
There is a trade-off I discuss with every new buyer: sampling adds one or two weeks up front, but it removes the risk of an entire leaking shipment. I have never seen that trade go the wrong way.
Yes. Any reputable PET bottle supplier will provide physical samples before bulk production. Request bottles and caps together, then test application torque, removal torque, vacuum leak performance, and line compatibility with your actual product fill. A hand-tight fit alone cannot confirm a leak-proof seal.
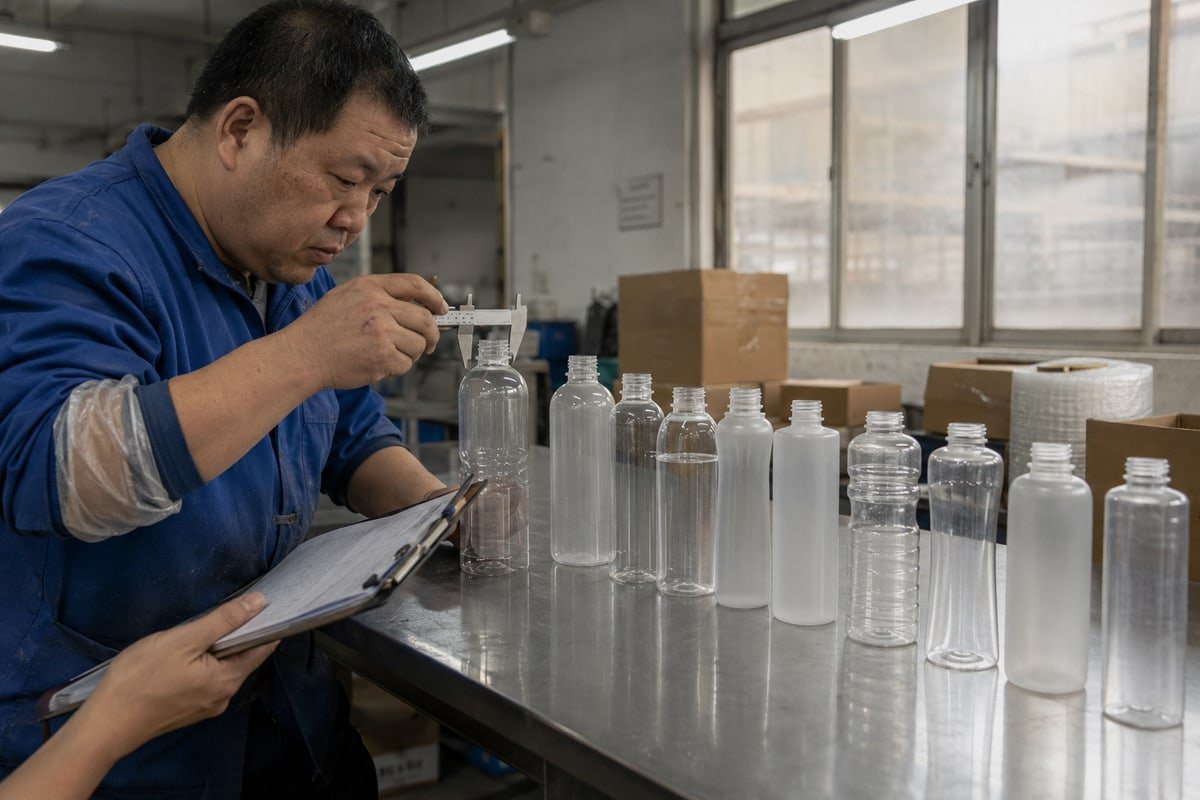
At our factory, we treat sampling as a required gate, not a courtesy. When we ship samples to clients in the United States, Germany, or Australia, we send the bottle, the cap, and the neck drawings together, so the buyer can run a full validation. Here is the sequence I recommend.
- Confirm the paperwork first. Match the neck finish code and closure part number on both drawings before touching the samples.
- Measure the samples. Repeat the caliper checks from earlier and compare against the drawings, not just against each other.
- Apply caps at target torque. Use your capper or a torque meter, not just your hand.
- Check removal torque after 24 hours. A practical rule of thumb: removal torque should land around 50–80% of application torque. Much lower suggests thread slip; much higher suggests liner sticking.
- Run leak-proof testing. A vacuum leak test on filled, capped samples reveals bypass leakage that a visual check misses. Inspect the land area — the flat top rim — for flatness and width, since the liner needs a smooth surface for a hermetic seal.
- Stress the seal. Thermal cycling matters, because caps that seal at room temperature can loosen in a hot container or a cold warehouse.
| Test | What it catches |
|---|---|
| Application/removal torque | Loose caps, cross-threading, thread slip |
| Vacuum leak test | Liner bypass, land area defects |
| Thermal cycling | Seal failure during shipping and storage |
| Line trial with product fill | Capper alignment, high-speed torque variance |
One more detail buyers overlook: liner material selection. A foam liner, an induction seal, and a plug seal each behave differently with the same neck. Test with the liner you will actually use, filled with your actual product. Personal care formulas with oils or surfactants can attack some liners over shelf life.
How do I work with my supplier to fix neck-to-cap sizing errors quickly?
The hardest lesson from my early years in this business: a sizing problem reported with photos and numbers gets solved in days, while a problem reported as "the caps don't fit" drags on for weeks.
Share caliper measurements, photos, and both neck drawings with your supplier immediately. Identify whether the error is a finish-code mismatch, a tolerance drift, or a liner issue. Then agree on a corrective plan — mold adjustment, replacement caps, or re-sampling — with a written timeline before production continues.
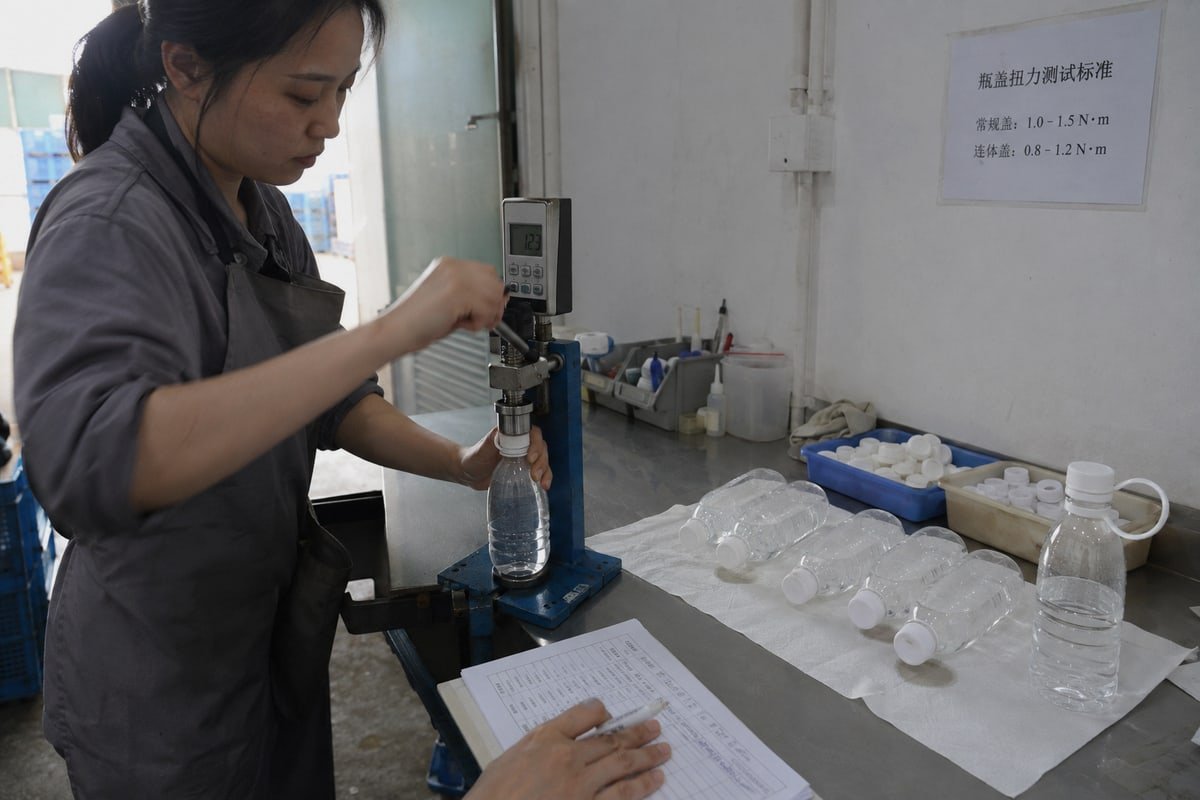
Speed comes from diagnosis, not pressure. When a client of ours reports a fit problem, the first thing our team asks for is data: T, E, H, and I measurements from at least five bottles, the cap part number, and a short video of the failure. With that in hand, we can usually classify the root cause within a day.
The three root-cause categories
Most sizing errors fall into one of three buckets. Each has a different fix, which is why the diagnosis step matters.
| Root cause | Typical sign | Fastest fix |
|---|---|---|
| Finish-code mismatch | Cap spins freely or bottoms out early | Replace caps or bottles with the correct series |
| Tolerance drift | Some bottles seal, others leak | Adjust or re-cut the mold; tighten incoming QC |
| Liner or land issue | Threads fit, but product still leaks | Change liner material or fix land flatness |
Use tolerances as the shared language
Vague complaints stall negotiations. Numbers move them. In practical guidance we share with buyers, workable targets look like this: neck outer diameter within ±0.10–0.20 mm, neck height within ±0.15–0.30 mm, thread position within ±0.15 mm, sealing surface flatness within 0.10–0.20 mm, support ring position within ±0.20 mm, and tamper-ring locking diameter within ±0.10–0.20 mm. Treat these as operational guidance, not universal law, but put agreed values into the purchase contract. When both sides sign the same tolerance sheet, "out of spec" stops being an argument and becomes a measurement.
Remember also that a PET neck is formed in the preform mold 4, not during blowing. So if the neck itself is wrong, the fix traces back to bottle preform specifications, and your supplier needs to check the preform tooling, not the blow mold. Knowing this helps you ask the right question and skip a week of back-and-forth. Finally, agree on corrected samples before restarting mass production, and confirm replacement logistics — for our DDP clients, we build the re-sample shipment into the recovery timeline so the launch date survives.
Conclusion
A mismatched neck ruins margins faster than any freight delay. Match the finish code, measure the T dimension, test real production samples, and lock agreed tolerances with your supplier in writing.
Footnotes
1. Global standards organization that develops technical testing methods for packaging integrity and seals. ↩︎
2. Official industry body providing the standardized neck finish specifications mentioned in the article. ↩︎
3. Official European Union legal database providing the text for the mentioned plastic packaging directive. ↩︎
4. Technical reference for the injection molding process used to create the bottle’s neck. ↩︎
